PRESS RELEASE 2013-10-14
A Difficult Problem with Threading
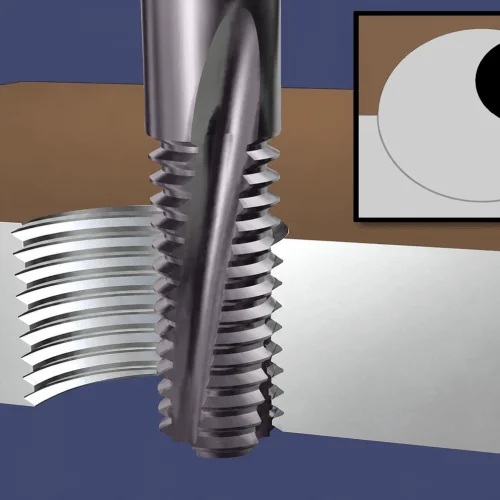
Burrs are always a difficult problem when threading. It doesn´t matter which method is used. The burrs must be removed. Chamfering is the most common method. As a standard tool solid carbide thread mills from SmiCut (ThreadBurr) deburr the thread on the top in the same operation as threading. Read more about ThreadBurr.
But what if the burr is at the back of the piece and the surface is not even and vary several millimeters. Hand Deburring is often applied. This is very time consuming, especially if it is a difficult to machine material.
The Solution for Removing Burrs Easily
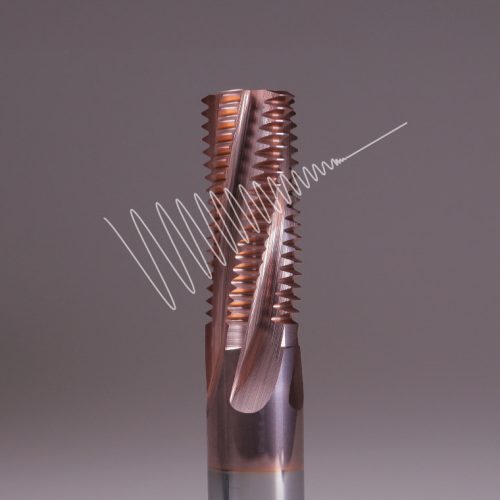
SmiCut has the solution to this problem. Thread milling with Double ThreadBurr. This milling cutter not only remove the burr on the top of the thread, but also on the back, and in addition it mills the thread.
An example is a thread on a turbocharger to the automotive industry in China. Before tested SmiCut’s thread mills, conventional thread milling cutters was used and hand deburring tools thereafter. Now Double ThreadBurr from SmiCut is used (see picture).

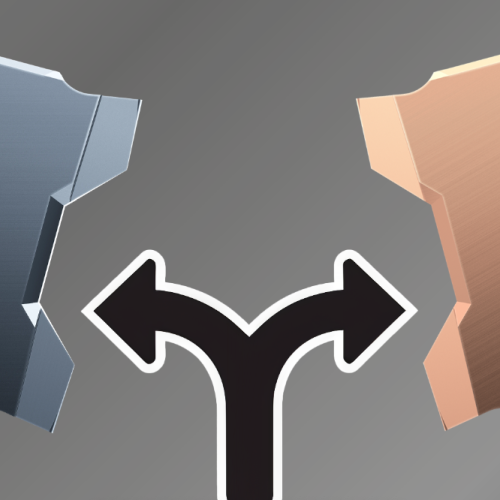
Double ThreadBurr deburr on both sides.
The customer was extremely pleased to avoid the time-consuming hand deburring. Deburring is automatic on both the top and bottom when thread milling with SmiCut’s Double ThreadBurr. No extra time for deburring. Threading and deburring is done in the same operation.
Extremely Long Tool Life
The most impressive was the extremely long tool life, 8 hours. The previous thread milling cutter managed 300 threads per cutter. They thought it was okey until SmiCut got 1300 threads per cutter. This is important because consumption was 600 thread mills per year. Now suddenly needed only 140 mills per year.

The thread on the top has no burrs

The thread on the back has no burrs